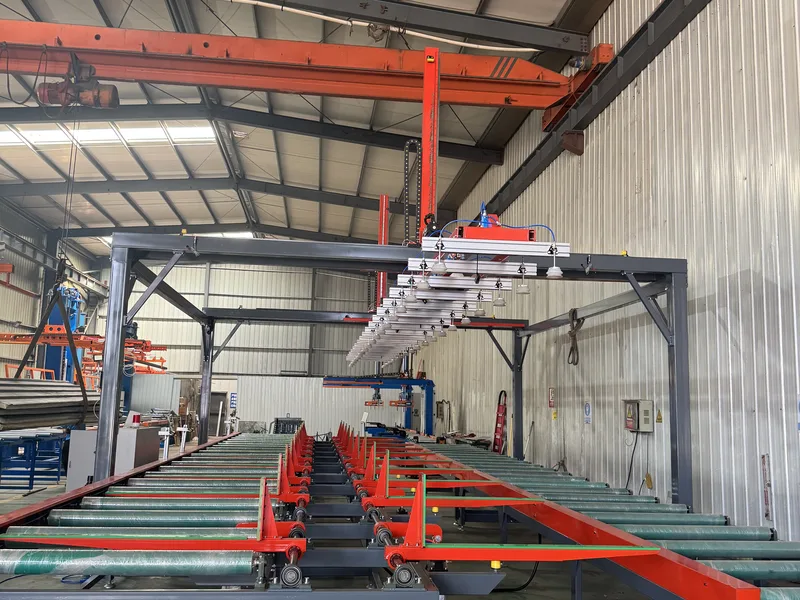
What should a gantry stacker acceptance test establish?
The test should establish whether the delivered configuration meets the signed project specification for the agreed panels and workflow. Agree samples, test scope, measurable criteria and evidence before the factory acceptance test (FAT). A brochure maximum or a short demonstration video is not an acceptance protocol.
This checklist is a preparation aid. It does not prescribe safety tests, alarm thresholds, structural checks, operating settings or universal pass limits. The supplier's engineering team and the buyer's responsible personnel must agree machine-specific procedures and requirements.
What happens before handover?
- Agree the scopeIdentify the ordered configuration, panel samples and criteria in the project protocol.
- Record the agreed reviewKeep sample IDs, actual results and supporting evidence together.
- Resolve open itemsDocument limitations, responsible reviewers and outstanding actions.
- Document handoverRecord shipment authorization and any separate site commissioning scope.
Preparation sequence only. This page supplies neither machine-specific test instructions nor approval to ship.
Which configuration and samples should be recorded?
- Machine identification, drawing revision, software/recipe revision and tooling configuration.
- Each ordered panel family: profile, contact face, coating, film, length, width, thickness and measured mass.
- Agreed longest, shortest, heaviest and thickness-extreme samples, including any combinations not tested.
- Required turnover orientation, stack arrangement and finished-stack handover point.
- Scope supplied by the stacker vendor versus equipment supplied by the line integrator or buyer.
For S04, use the English product PDF as configuration context: 4–15 m panels, 50–200 mm thickness, stated 450 kg total load, 24 cups and 0–2,000 mm stack height. Confirm the ordered limits in writing; these maxima do not validate every combination.
What should the acceptance record contain?
Pickup
Identify the sample and contact face. Reference the agreed requirement and actual handling observation.
Required turnover
Record the agreed orientation and whether turnover is included for this sample.
Placement & surface
Link the placement result and before/after contact-area observations to the sample ID.
Stack & handover
Record the agreed stack arrangement, count and responsibility for completed-stack removal.
Conceptual handling sketches. They do not show a tested machine, approved cup layout, operating procedure or pass result.
| Review item | Evidence to agree and record |
|---|---|
| Panel handling | Identified sample, pickup face, intended motion and placement result; limitations noted. |
| Surface condition | Before/after observations of agreed contact areas and protective film against agreed criteria. |
| Cycle and representative run | Timing boundaries, individual cycles, sample mix, accepted count and interruptions. |
| Stack formation and discharge | Stack arrangement, counting, full-stack handover and responsibility for removal equipment. |
| Controls and changes | Agreed interfaces, recipe identification, changeover scope and training records. |
| Machine-specific safety documentation | Responsible reviewer, applicable documentation and approved protocol; use the supplier's procedures, not this web checklist. |
| Handover | Delivered-machine manuals, drawings, parts list, outstanding actions, ownership and sign-off. |
How should the cycle-time claim be checked?
Define the start and finish events and confirm whether turnover, placement and return readiness are included. Record interruptions separately. S04's stated 20–30 seconds per panel is nominal; a project acceptance criterion must specify the relevant panels and conditions.
Use the cycle-time and line-speed guide to distinguish handling time from arrival intervals and sustained output. Test the agreed stack-change and discharge arrangement as part of the relevant scope, not as an assumed included feature.
Download the acceptance preparation record
How does the blank record work?
- Before the review
- Add the agreed requirement, panel sample or configuration and responsible reviewer.
- After the agreed review
- Add the actual result and evidence reference. Keep any untested case visible.
- At handover
- Record outstanding actions and status or sign-off by the responsible person.
CSV spreadsheet with 16 review items. No pre-filled limits, test results or approval.
Open the blank record in a spreadsheet. Add the agreed requirement, responsible reviewer, actual result, evidence reference and outstanding action. The file contains no pre-filled pass criteria or approvals. For a print copy of this guide, use your browser's Print command.
Before shipment
Resolve or explicitly document outstanding actions and limitations. Record who authorizes shipment and which tasks remain for site installation or commissioning. FAT does not automatically establish site acceptance.
Common acceptance questions
Does the 41-second product video prove acceptance?
No. The video on the product page shows the machine, but does not establish test load, representative output or signed acceptance.
Can this checklist replace an operating manual?
No. Only delivered-machine documentation and approved procedures should be used for operation, maintenance and safety-related testing.
What if an extreme panel was not available at FAT?
Record the untested case and agree how suitability will be confirmed. Do not sign an untested product family off by analogy without the responsible team's approval.
Review your gantry stacking project
See the Automatic Gantry Flipping & Stacking Machine for Sandwich Panels and download its English product specification. Send the actual panel drawings, mass and line conditions for configuration review.
Send project requirementsUpdated · Prepared by Color Steel Machine. Configuration basis: the supplied manufacturer product document and confirmed 50–200 mm thickness range, reflected in the English product PDF. General planning guidance, not an operating or safety manual. The signed project specification and delivered-machine documentation govern.